What Is an Aluminum Machining Part?
An Aluminum Machining Part is a component shaped from aluminum stock through controlled cutting processes. It may begin as a plate, bar, tube, or near-net-shape blank. CNC mills, lathes, and drilling tools remove material with measured precision. The result can be a bracket, housing, spacer, connector, or custom structural piece. Simple in appearance. Its performance depends on more than its bright surface.
Aluminum is valued for its low density, corrosion resistance, and practical machinability. Different alloys behave differently under cutting, heat, vibration, and finishing. For example, 6061-T6 often suits general structural components, while 7075-T6 offers higher strength with different manufacturing considerations. A reliable supplier checks drawings, tolerances, tool access, burrs, and surface requirements before production. Measurements should be verified with calibrated instruments, not visual confidence alone. That detail matters.
This article explains how an Aluminum Machining Part is designed, produced, inspected, and selected for real applications. It also considers cost, lead time, alloy choice, and finishing options. Practical experience shows that a tight tolerance is not automatically a better specification. It may increase machining time without improving service performance. That is worth questioning. Readers will find clear terminology and realistic guidance for discussing parts with engineers or manufacturers. Still, every application has limits. Load, temperature, environment, and assembly conditions must be reviewed before approval.
Definition and Core Characteristics of an Aluminum Machining Part
What Is an Aluminum Machining Part?
Definition and Core Characteristics of an Aluminum Machining Part
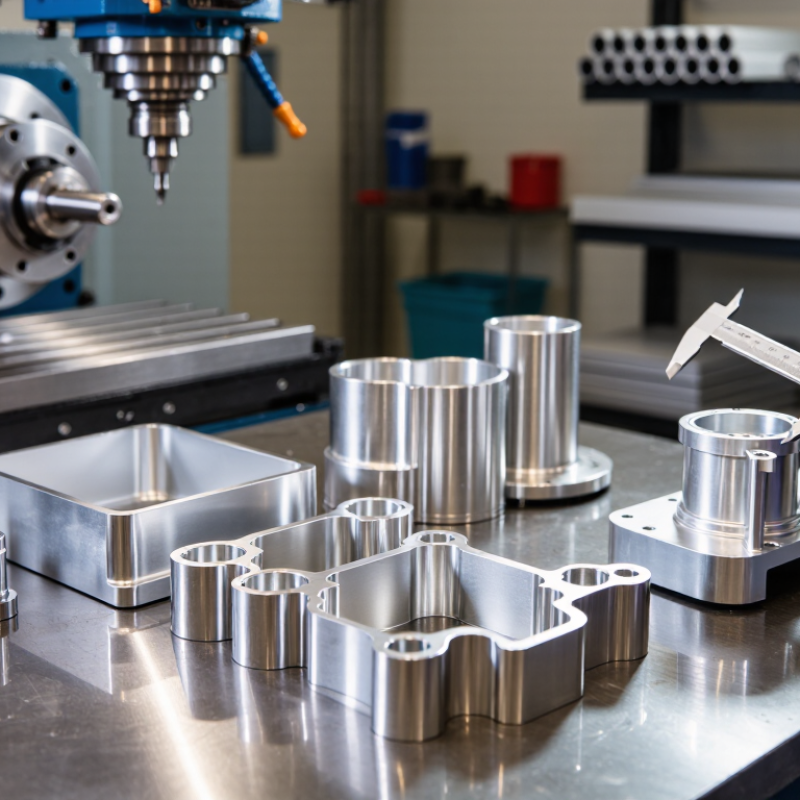
An aluminum machining part is a component shaped from aluminum stock through controlled cutting operations. A machine removes material until the part matches a technical drawing or digital model. Common operations include milling, turning, drilling, tapping, and reaming. The result may be a small spacer, housing, bracket, shaft, or precision fixture.
Its core characteristics begin with low weight and useful strength. Aluminum also transfers heat efficiently and resists corrosion in many environments. Its natural machinability supports clean cuts and relatively fast production. However, it is not automatically easy to machine. Thin walls can vibrate, and sharp tools can leave burrs or smeared edges. These details matter.
Dimensional accuracy is another defining feature. Critical holes, flat surfaces, and bearing seats may require tight tolerances. Surface finish depends on tool condition, cutting speed, coolant control, and material grade. Experienced machinists inspect parts with calipers, micrometers, gauges, or coordinate measuring equipment. They also check threads, edge condition, and distortion after clamping.
Design affects the final result. Deep narrow pockets may trap chips and increase tool deflection. Very small internal corners may require special cutters. In practice, a drawing can appear reasonable but still create production problems. Reviewing tolerances early often prevents rework. Anodizing or another protective finish may improve appearance and surface performance, but it can slightly change dimensions. That adjustment is easy to overlook.
What Is an Aluminum Machining Part? - Definition and Core Characteristics of an Aluminum Machining Part
| Dimension | Core Characteristic | Typical Data or Range | Practical Significance |
|---|---|---|---|
| Definition | A component produced by removing material from an aluminum workpiece using cutting tools or abrasive processes. | Common processes include CNC milling, CNC turning, drilling, tapping, reaming, and grinding. | Allows accurate production of housings, brackets, shafts, plates, fixtures, and other engineered components. |
| Material Composition | Aluminum machining parts are usually made from wrought aluminum alloys containing controlled amounts of elements such as magnesium, silicon, copper, zinc, or manganese. | Aluminum content is commonly above 90% by mass, depending on the alloy family. | Alloy selection affects strength, corrosion resistance, machinability, weldability, and surface finish. |
| Density | Aluminum has a relatively low density compared with steel and many other engineering metals. | Approximately 2.66–2.85 g/cm³ for common wrought aluminum alloys. | Parts can be significantly lighter than steel equivalents, supporting weight reduction in machinery and transport applications. |
| Strength | Mechanical strength varies substantially with alloy type and temper condition. | Typical ultimate tensile strength is approximately 120–570 MPa for commonly machined wrought alloys. | The selected grade and temper must match the required load, fatigue performance, and dimensional stability. |
| Machinability | Many aluminum alloys are relatively easy to cut because of their low density and moderate hardness. | High cutting speeds are commonly possible, subject to tool geometry, rigidity, cooling, and alloy condition. | Efficient machining can reduce cycle time, but built-up edge and chip control must still be managed. |
| Thermal Conductivity | Aluminum transfers heat efficiently from the cutting zone and from operating components. | Approximately 120–235 W/m·K for many commonly used wrought alloys. | Good heat dissipation is useful for heat sinks, enclosures, and thermal-management components, but cutting temperatures can change quickly. |
| Corrosion Resistance | Aluminum naturally forms a thin oxide layer that helps protect the surface from further oxidation. | Generally good in many atmospheric environments; performance depends on alloy, surface condition, and exposure. | Suitable for many outdoor and industrial applications, although harsh chemicals, galvanic contact, and saltwater may require added protection. |
| Dimensional Accuracy | CNC machining can produce close tolerances when the machine, tooling, workholding, and process are properly controlled. | General CNC tolerances are often around ±0.05 mm; tighter tolerances require specific process control and inspection. | Tolerance requirements should be specified only where functionally necessary to control cost and manufacturing risk. |
| Surface Finish | Machined aluminum can provide a clean, reflective, or satin surface depending on tooling and finishing operations. | A typical CNC-milled finish may be approximately Ra 1.6–6.3 µm; finer finishes require additional control or finishing. | Surface requirements influence tool selection, feed rate, cutting strategy, and post-machining treatment. |
| Common Alloy Families | Different alloy families provide different balances of machinability, strength, corrosion resistance, and weldability. | Common families include 2xxx, 5xxx, 6xxx, and 7xxx series wrought alloys. | 6xxx alloys are widely used for general machining; 2xxx and 7xxx often provide higher strength; 5xxx alloys are valued for corrosion resistance and weldability. |
| Typical Machining Operations | The final part geometry determines the combination of material-removal operations. | Facing, pocketing, contouring, slotting, drilling, boring, tapping, turning, and chamfering are commonly used. | A suitable process sequence improves accuracy, tool life, chip evacuation, and production efficiency. |
| Post-Machining Treatments | Additional treatments can modify appearance, hardness, wear resistance, or corrosion performance. | Common options include anodizing, chemical conversion coating, powder coating, painting, polishing, and bead blasting. | Treatment selection should consider dimensional change, electrical conductivity, service environment, and appearance. |
| Typical Applications | Aluminum machining parts are used where low weight, corrosion resistance, thermal performance, and precise geometry are important. | Examples include equipment frames, robotic components, electronic enclosures, heat sinks, vehicle parts, fixtures, and prototypes. | The final design should balance material properties, tolerances, manufacturability, operating conditions, and total cost. |
Note: Material properties and machining results vary according to alloy, temper, stock form, equipment, tooling, cutting parameters, and inspection method.